If you’ve ever spent time in a metal fabrication shop, woodworking studio, or even a home garage tackle a project that calls for non-round holes, you know the frustration of settling for a wobbly, inaccurate result. I’m Jesse, and for the past 12 years, I’ve sold drill presses to craftsmen, machinists, and DIYers who’ve come to me with that exact frustration. Most people think a drill press is only for perfectly centered round holes—but the truth is, it’s one of the most reliable tools for eccentric drilling, too. Eccentric drilling (cutting holes whose centers aren’t aligned with the axis of your drill bit) sounds fancy, but it’s how you make offset holes for bolt circles, custom hinges, or even decorative round shapes shifted off a workpiece’s core. Today, I’m walking you through exactly how to do this safely, accurately, and with consistent results—no trial and error, no ruined workpieces, just solid, actionable steps I’ve shared with hundreds of my customers over the years. Drill Presses

First, let’s get one thing straight: eccentric drilling isn’t the same as just clamping a workpiece off-center and drilling a regular hole. That method leads to drift, bit walk, and a lopsided hole that’s useless for precision work. We’re talking about controlled offset, math that’s simple once you break it down, and technique that turns a standard drill press into a tool for custom, offset cuts. Before we dive into the steps, let’s cover the basics you can’t skip—because safety and setup are make-or-break here.
First, confirm your drill press’s capabilities. Not every drill press can handle this, especially if you’re working with large offsets. When I help a customer pick a drill press for eccentric work, I check two numbers: the maximum travel of your quill (that’s the part holding the drill bit, which moves up and down to make the cut) and the distance from the quill’s axis to the column (the big vertical pole your drill head slides up and down on). For small offsets—say, 1/4 inch to 1 inch—most benchtop drill presses work fine, but for offsets over 1 inch, you’ll want a floor model with a larger head that can swing further from the column. I always tell folks: never push your drill press past its rated capacity. If your machine specs say maximum offset is 1.5 inches, don’t try to make a 2-inch offset—that’s a surefire way to bend a bit or damage your drill press.
Next, gather your core setup tools. You’ll need: a drill bit appropriate for your material (high-speed steel for metal, carbide-tipped for hardwood or dense composites), a good quality vise or drill press clamp (wobbly clamps equal to wobbly holes), a surface plate or the drill press table (it needs to be flat), a ruler or caliper for measuring, a center punch, a hammer, and most importantly, either a magnetic drill press offset attachment or a custom-made wooden guide block. Wait, a guide block—this is a trick I learned from a master machinist I worked with early in my career, and it’s way more reliable than freehand clamping. Let me explain: the guide block is a rectangular block of hardwood (like maple, which stays flat and doesn’t dent easily) cut to a size that fits in your vise, with a slot cut along one edge. The slot is positioned so that when you clamp the guide block to the drill press table, the offset distance you want is exactly between the drill bit’s axis and the edge of the block. That way, every time you slide your workpiece against the block, it’s at the exact same offset—no measuring mid-project, no human error.
Now, let’s get into the actual process, step by step, so it’s clear. The first step is always planning your offset. Let’s say you need to drill a hole that’s 1 inch off-center for a custom hinge on a cabinet door. First, measure the center of where you want the hole to be on your workpiece. Let’s call that point X. The center of your drill bit (let’s call that point Y) needs to be exactly 1 inch away from X. That’s your offset distance: 1 inch. Write that number down, because that’s what we’re working with.
Second, set up your drill press table and drill head. Loosen the table lock, and slide the table sideways until the distance from the drill bit’s axis (you can find this by marking the center of the chuck with a pencil) to the edge of the table is equal to your offset. Wait, no—if you’re using the guide block method, that’s even easier. Clamp the guide block to the drill press table so that the edge of the block is exactly at your desired offset. So if your offset is 1 inch, the block’s edge is 1 inch away from the drill bit. That means when you slide your workpiece tight against that block’s edge, the hole you drill will be exactly 1 inch off your workpiece’s center. Way simpler than moving the table every time, especially if you’re making multiple identical holes.
Third, mark your workpiece’s hole center. This is non-negotiable. Even with a guide block, you need to mark where the hole is going, and then use a center punch to make a small indent at that mark. Why? Drill bits have a tendency to walk, especially on hard materials. The center punch indent is a tiny guide that keeps the bit from sliding off the mark before the full depth of the hole is cut. For soft materials like pine, a small indent works; for metal, make it a little deeper with a steady tap of the hammer.
Fourth, adjust your drill depth. Most drill presses have a depth stop, which is a simple pin that you set to stop the quill from moving down once the bit has cut to your desired depth. For eccentric drilling, the depth stop is extra important because it keeps you from drilling too deep and accidentally cutting through the other side of your workpiece if it’s thin. Set the depth stop to the exact thickness of your workpiece plus 1/16 inch (to make sure you cut all the way through) and lock it in place.
Fifth, secure your workpiece and make the cut. This is where the guide block shines. Slide your workpiece tight against the edge of the guide block, making sure the center punch mark is aligned with the bit. Then clamp the workpiece to the table tightly—two clamps, one on each side, so it doesn’t shift mid-drill. Turn on your drill press, let the bit reach full speed, then lower the quill slowly and steadily. Don’t force the bit; let it do the work. For metal, use cutting fluid to keep the bit cool and prevent it from overheating; for wood, use a sharp bit to avoid splintering, and consider a backer board behind the workpiece to prevent tear-out.
Wait, what if you don’t have a guide block? That’s okay too— I’ve helped DIYers on a budget do this with just a vise and careful measuring. If you’re not using a guide block, the key here is to clamp your vise to the drill press table such that the distance from the drill bit’s axis to the edge of the vise’s jaw is equal to your offset. Then, place your workpiece in the vise, tight against the jaw, and make the cut. The downside here is that you have to remeasure every time you move the vise, and if you’re making multiple holes, you have to readjust every time. For small projects, it works, but for precision work, the guide block is worth the 10 minutes it takes to cut one.
Now, let’s talk about common mistakes I see people make all the time with eccentric drilling, and how to avoid them. First, using a dull drill bit. I can’t stress this enough— a dull bit will wander, skip, and leave you with a hole that’s off by 1/8 inch before you even finish. I recommend replacing bits every 50 to 100 holes, depending on the material, and always sharpening them properly if you’re reusing. Second, not clamping the workpiece tight. If the workpiece shifts even a tiny fraction of an inch mid-drill, your offset will be off. I once had a customer bring me a piece of custom furniture he’d ruined because his workpiece shifted, and the hole was so far off he had to re-drill the whole door. A second pair of clamps would’ve fixed that. Third, drilling too fast. High speed is great for small holes in metal, but for eccentric drilling, slower is better. If you’re working with a 1/2-inch bit in steel, run the drill press at half the speed you’d use for a centered hole. That reduces bit flex and keeps the cut accurate. Fourth, ignoring the drill press’s capacity. I’ve seen people with 10-inch benchtop drill presses try to do 2-inch offsets, and the drill head would rock, making the hole lopsided. Always check your machine’s maximum offset rating before you start.
Another advanced trick for eccentric drilling: making custom shapes, like offset circles or even small gears. If you want to drill a hole that shifts the center completely, not just offset a standard hole, you can adjust the method slightly. For example, to make a 2-inch diameter offset circle, you’d set the offset to 1 inch, then drill a series of overlapping holes around your desired center, then file or sand the edges smooth. It takes a little practice, but it’s a great way to make custom parts without a CNC machine. I sold a set of benchtop drill presses last year to a hobbyist who makes custom wooden clock gears, and he uses this trick for every single gear he makes—says it’s saved him thousands of dollars in tool costs.
Now, safety, which I always emphasize to every customer, no matter how experienced they are. Eccentric drilling puts a little more strain on your drill press and your bit, so you need to take extra precautions. Always wear safety glasses—never skip this, even if you’re just making a small hole. Wood chips and metal shavings can fly at high speed, and they’re sharp enough to cause a serious eye injury. Never wear loose clothing, gloves, jewelry, or long hair that could get caught in the drill bit. If you have long hair, tie it back up into a bun or under a hat. Also, never reach over the drill press while it’s running, and never remove chips with your hands while the bit is spinning—use a brush. And if you’re using a magnetic offset attachment, make sure it’s properly seated before you start, because a loose attachment can come flying off mid-drill.
Let’s wrap this up with a quick real-world example, something I did just last month to make a custom shelf for a customer. The shelf needed four offset holes for metal brackets, each 3/4 inch off the edge of the shelf. I grabbed a 12-inch benchtop drill press (great for small woodworking projects), a sharp 5/16-inch wood bit, a maple guide block I cut that day, a center punch, and a pair of clamps. I measured 3/4 inch from the drill bit, clamped the guide block to the table, marked each of the four hole positions on the shelf, tapped them with the center punch, clamped the shelf tight against the guide block, set the depth stop to 1/2 inch (the thickness of the shelf), and drilled each hole. All four holes were exactly 3/4 inch off, no errors, no sanding needed. The customer loved it, and it took less than 10 minutes. That’s the beauty of eccentric drilling with a drill press—it’s precise, fast, and accessible for almost anyone, as long as you follow the steps.
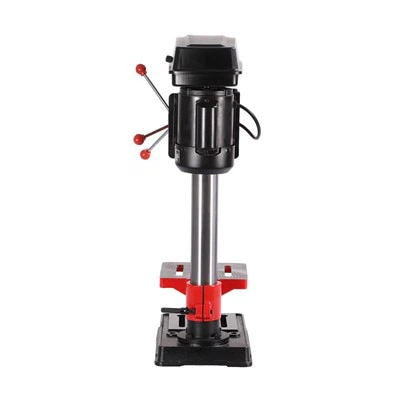
If you’re ready to try eccentric drilling for your next project, or if you need a drill press that’s right for your work—whether it’s small woodworking, metal fabrication, or large-scale machinist projects—we’re here to help. We carry a full line of benchtop and floor drill presses, plus all the attachments and accessories you need for eccentric drilling, and our team can walk you through setup and techniques to make sure your projects turn out perfect every time. To talk through your specific needs, just reach out to our sales team to start a conversation and get recommendations tailored to your work.
CNC Metal Lathe References
Machinery’s Handbook, 31st Edition: A Reference Book for Mechanical Engineers, Draftsmen, Machinists, and Metal Workers
Drill Press Operation and Safety Guidelines, Occupational Safety and Health Administration (OSHA), 2022
Woodworking Machine Techniques: Drill Press Operations, Fine Woodworking, 2021
Metal Fabrication Basics: Precision Drilling for Custom Parts, Fabricator Magazine, 2020
YS Machine Tools Co., Ltd.
We’re well-known as one of the leading drill presses suppliers in China, featured by quality products and good service. Please rest assured to buy customized drill presses at competitive price from our factory. Contact us for more details.
Address: 300 Sandusky st, Ohio, 43611, USA
E-mail: yishoumachinetools@gmail.com
WebSite: https://www.ysmachinetool.com/
